G71 is sometimes known as a canned cycle when in fact it is a multi repetitive cycle. The G70 cycle goes with it and can pick up the same lines to finish.
The N numbers are important as the cycle uses these as the points of reference to jump to.
G71 cycle interprets the shape between these two N numbers and then breaks up the shape for roughing.
Basic Turning, in the early days of CNC Turning G96 was one of the things that really made a massive difference.
It meant that instead of having to turn a part at a fixed speed and feed, the part could be programmed in G96 which was a constant surface speed.
Where diameters changed, particularly when facing, it made a massive improvement to tool life and surface finish as well as speeding up the whole process.
G97 Speed In RPM
In Basic Turning when you program G97 your machine will start the chuck up at a speed in RPM. So if you program. G97 S1500 M3
Your chuck will start revolving clockwise at 1500 rpm.
G97 for Drilling Tapping and Screwcutting
When drilling a hole you are on the centreline of the machine so you just want plain old simple RPM.
G96 however means meters per minute. This is a surface speed. G96 S200 M3
Your machine would start up at a surface speed of 200 meters a minute. Now your RPM would depend on where on the diameter the tool was positioned.
If the tool was positioned at a 100mm diameter it would be as if the tool were able to run around this diameter at a speed 200 meters a minute.
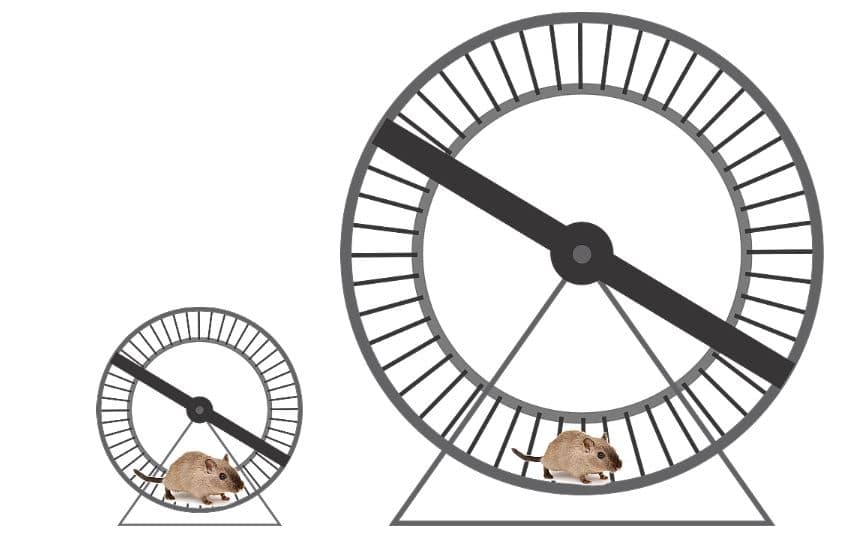
It’s a bit like being on a running machine if you ran at 200 meters a minute and placed various diameters under your feet the large ones would turn at slow rpm and the small ones would turn at high rpm. (Just like the hamsters above)
That’s why on a manual lathe it is hard to face a large diameter without changing speed half way.
Neeeeeoooooooowwww
You know when you face a part on a CNC Lathe and you hear that change in pitch? It’s the spindle increasing in RPM as it gets closer to the center of the part.
Well I bought my hamster loads of different wheels to play on just like the one above.
My hamster suffered with depression on account of being stuck in a cage all day and not having a girlfriend oh and he had a lot of credit card debts too.
These wheels varied in diameter from about 6 inches to a massive 2 foot one. They kept him happy all night. He was so tired he slept all day.
Harold could only run so fast but I noticed when he was on the small 6 inch wheel it absolutely whizzed around. Now on the big two foot diameter one it took him ages just to get it to spin around once.
G96 G97 all about hamsters
Harold Had G96
A CNC machine in G96 will give a lovely finish because the surface speed always remains the same.
So even though Harold ran at 200 metres a minute (this is fuckin lightening speed for a hamster)
The wheels ran at different RPM depending on what diameter they were.
Harold Was a Clever Bastard
Oh by the way Harold had a tail (unlike other hamsters) and a maths qualification.
He knew that if he multiplied the diameter of the wheel by .00312 it would give him the circumference of whatever wheel he was running on in meters.
200 mm wheel (.00312 x 200 = .6864)
All he now needed to do was divide this answer into the speed he was running at and he would know how many RPM his wheel was revolving at.
If he was running at 200 meters a minute not only would he be fuckin knackered but the wheel would be running at 291 rpm
200 / .6864 = 291
Basic Turning Manual Machining
Using a manual machine you have to compromise. At the outside your speed is too fast and when you get to the centre you are too slow.
Manual Lathe
On a CNC lathe we would normally program in mm per revolution as well because the speed is changing all the time so we need our feed to be locked into the speed.
With a machining centre our cutter is always revolving at the same speed so the feed can be constant in mm per minute.
Someone out there will be thinking “what happens in G96 when you get to the centre of the part”. Well the spindle will be flat out!
See how surface speeds are translated to speeds in RPM. There are many converters online that you can use for this and I do recommend their use. It will also mean you don’t have to watch my tedious video.
When I train people at the CNC Training Centre my emphasis is on understanding not memorising. I usually start by saying “please don’t remember all the things I am telling you”.
In the early days training students in Basic Turning I remember them saying to me the next day that they had G codes floating around in their head from the lessons the day before.
G96 and G97
What I really mean is that the most important thing is to understand what the machine can do and the concepts of programming and Basic Turning.
You could say “I know there is a G code that makes the machine run in RPM” so all you need is a list of G codes.
If you can be bothered to work through the simple maths above. It will help you to fully understand how G96 is works.
G92 threading Cycle is something that concerns me. It’s sadly neglected. Now I know you’re probably saying “no one uses that old shit anymore”
Well you could be wrong.
G92 Threading works exactly the same as G76 except you need to programme every pass. This would be a pain in the arse but hear me out.
The Haas G76 cycle does not have any facility for a spring pass. This is where you add extra cuts at the end of a threading cycle to take out any metal left from the tool pushing off.
On a Fanuc control you can put these extra spring passes in as part of the G76 cycle.
It’s been a while since I trained anyone on a Mazak Quick Turn Machine. Another training job completely out of the blue.
Custom Rifles, didn’t know what to expect really. Anyway a drive to Tunbridge Wells, where for the price of a garden shed you could probably buy my village in the Midlands.
I ended up in glorious countryside on a farm in what felt like the middle of nowhere. The guy who runs this company (Paddy) has his workshop in the outbuildings of the farm.
It is like walking into Dr Who’s Tardis. This workshop wants for nothing, surface grinding, shot blasting. This guys even got a Faro Arm!
Two Haas machines and the Mazak Quick Turn 10. Not the tidiest of workshop but I am told it’s a work in progress.
It is really heartwarming to see such investment in tooling and modern equipment in what effectively is a one man band.
Paddy is a brilliant engineer and mostly self taught. Loads of the CNC stuff learnt from my website (happy days) . This guy googles everything but not in a “What I had for breakfast, oh fuck the cat just threw up” type of way.
This is very constructive use of google definitely the way forward.
He already had a pretty good understanding of what the machine could do. Being self taught, several gaps in his knowledge, so, in steps me, to fill em all up.
Paddy rebuilds, repairs and creates custom rifles.
Mazatrol
I had forgotten just how brilliant these machine are. I don’t believe there is a quicker way to get a part from drawing to bubble wrap than the Mazak Quick Turn.
Check out this video on Tool Path Store another brilliant feature on the Mazak Quick Turn.
I’m not flogging these things by the way but if your reading this article I’m always open to offers. That is providing I keep my clothes on, well maybe not, how much we talking?
From its original concept Mazatrol has never really got much better and that’s not a criticism. For turning it’s just bloody good, very bloody good.
Like for example on a Mazak you index the turret and you wanna use a tool. Now that’s not a big ask is it?
Well on most other controls you can’t because the bloody offset is not active. You can call it in MDI if you want. That is if you know how. Trouble is, the minute you press RESET it’s gone .
On a Mazak once you index the turret that tool is active along with all its associated geometry.
That means you can start manual turning with hand wheel or jog and the diameter is what it says on the screen.
So simple, so obvious but what a difference it makes. The list goes on and on as to how well thought out these Mazak Quick Turn machines are.
All the information is saved with the program. So that means your work offset, jaw details and chuck details are all there when you call the program again.
Graphics
Now the graphics are not like“Assassin’s Creed Origins” but they are adequate and definitely help a lot. If you can be arsed to set the graphics up with chuck jaws n stuff then you can be certain all will be okay when you run it for real.
You can even jump from the program directory straight to a graphic simulation of the part so there is no “oh shit I wish I’d made a note of what this does” moment. You quickly get to see what the program does.
Footnote: You should still add a program description (and there’s a facility for this too.)
Liar Liar Your Bums On Fire
One of the main criticisms I hear of Mazatrol is that you have to “Lie to it”. I think when you want to do something a bit unusual it’s sometimes hard to get Mazatrol to do it.
This Mazak Quick Turn 10 is a two axis CNC Lathe. Let’s be honest most of the bits you make are gonna be quite simple. If not then this is where the Manual Programming Unit steps in.
Manual programming units are the Mazak “Get Out Of Jail Free” card
You can go back to some very crude G code programming within Mazatrol. These Manual Programming Units can sometimes get you out of a jam. It is quite limited, in what G codes you can use, but it will help a lot.
Incremental is a bit strange because it does not use U and W like you would normally on a Fanuc type system. It puts like a sign after your X or Z to tell you it’s incremental.
Need To Know
It’s well documented how easy it is to program in Mazatrol so I won’t dwell on it.
If you have never used Mazatrol you need to check it out. I think it is the epitome of “need to know”. What I mean by that is that it’s the minimum amount of information to get it to make some bits.
You know stuff like do you want tool nose radius compensation? Of course you bloody do. So it doesn’t ask you, you just get it.
Anyone who has only used Mazatrol probably wouldn’t know what you were on about. And why should they care?
It’s like knowing all the bits inside your telly who gives a shit when you just want to watch “Emmerdale Farm”. I don’t watch that crap by the way, honest.
Read On It’s Not All This Boring
This control can smoothly go into ISO programming. Not sure if this is an option but they all seem to have it.
So………. from a Mazatrol program you just jump into an ISO G code type program and everything works the same.
So what’s all the fuss about. If there’s something you can’t do in Mazatrol just write a bit of straight ISO G code type program and call it from your Mazatrol main program. So there you go job done stop whining.
Even the graphics work in ISO so there is no excuse.
Priority
When you finish your program you get this list of processes and you can really easily swap things around. You know like if you wanted to thread before you did the grooving, you can easily just swap the order.
Then you have this button that says Rough Priority. When you press it all the roughing is done first. How cool is that??
Program Restart
It always amazes me that CNC Machines are never that good on this. Well Mazaks are not bad actually.
You can really easily start from any program unit in Mazatrol. It’s also got this Single Process thingy that’s been around for years. Dead useful though. It means you can just run one unit, so you don’t have to worry about it carrying on to the next unit it just does that unit and ends.
Useful for stuff like just going over a thread again.
You can’t actually break into a unit to restart but on CNC Lathes you nearly always just want to start at the beginning of a tool.
If you have an ISO program it’s still better than a lot I could name. A bit convoluted in a way only the Japanese seem to be able to do. Nevertheless seven out of ten.
Procrastination
I was accused of this years ago and once I’d looked it up I thought yea that’s me. “What’s the point of this you ask? He’s off again”
When you are running an ISO program and you are milling say a shape or something. You look at the program and you see something coming up that you never got round to changing. It could be a feedrate or something.
It’s something that can keep pissing you off cos you forget to do it.
Help is At Hand. On a Mazak you can actually go into edit and alter it then come back n continue your program.
I just love showing people that one, makes me feel like I earned my money.
Oh yea by the way this is only when you are in an ISO program not Mazatrol
Things I Don’t Like
Take That Records
Beef Burgers
Brass Bands
No I meant about this machine Mazak Quick Turn.
Not much actually, oh the editing is a bit slow.
Editing
Editing in ISO is a doddle.
Editing in Mazatrol is very cumbersome and when it comes to stuff like copying a unit you have to say what program it’s from and all sorts of bollocks. It wants your bank account number and sort code.
There are more questions than a fuckin mortgage application.
Moving units is the same not a pleasant customer experience. Once you get used to it and how the Mazak brain is wired it’s ok though.
Let’s Be Honest
There ain’t much to not like about the Mazak Quick Turn.
Even if I were only going to use the machine is ISO (Fanuc type programming) and not use Mazatrol I would still seriously consider buying one of these machines.
Why…..
In ISO it’s easier to restart a program than most G code controls.
The editing is easy.
Better graphics than most. (It’s still like early space invaders)