G76 Threading Start Point (Where Do you Start?)

Tags :

Category : Fanuc Turn

G76 threading start point, when you use a G76 threading cycle on a CNC Lathe the position that you start the tool at is really important.

This is the position you rapid the tool to just before you call the G76 threading cycle.

For example how does the control know if you are producing an internal thread or an external thread.

Actually I learnt this the hard way. It was on an old machine.

G76 threading start point

Maybe not that old. Anyway I couldn’t get it to perform a G76 threading cycle. It was cutting an external thread but the tool was working it’s way outwards.

What to do Next?

Everything rushed through my head, senile dementia, flashbacks from a misspent youth, did I feed the dog?

Anyway I suddenly realised I didn’t have a dog and that the start position of the tool was wrong.

G76 threading start point how was it wrong?

Well that’s how the machine knows whether you want an internal or external thread. Your start point needs to be inside or outside the thread. What a fuckin dipstick I was.

I had the tool just below the external diameter of the thread. If you do this the machine thinks the thread is internal and therefore cuts outwards.

Correct

G76 threading start point

So providing the tool is initially placed outside of the maximum diameter it will do exactly what you want.

IncorrectG76 threading start point

Put it here and you are in deep shit. The tool will work from this position backwards and you will be totally confused.

Don’t say I didn’t warn you.

Here is a example of a 20mm external thread.

G0 X21. Z3.
G97 S1200 M3

G76 P010060 Q20 R.02
G76 X16.93 Z-25. P1535 Q485 F2.5

This thread has a core diameter of 16.96 (X16.93) the thread depth is 1.535 (P1535).

Soooo…… 16.93 + (1.535 x 2) = 20

G76 threading start point

Therefore you must first position the tool outside that 20mm diameter.

If you don’t do this then your tool will try and cut away from the 20 mm diameter.

Wrong as Below

G0 X19.95 Z3.
G76 P010060 Q20 R.02
G76 X16.93 Z-25. P1535 Q485 F2.5

So be careful because you might not notice that tiny amount.

Of course if you have a Siemens control Sinumerik 828 840D then this does not apply because you have to specify if the thread is internal or external in the cycle.

Front Clearance (G76 threading start point)

Now let’s think about how far in front of the part you need to be with the threading tool.

Maybe you never thought about it?

Well now’s the time.

Spare a thought for people like me who lie awake at night ruminating about these things. If you don’t know what ruminating means then maybe you shouldn’t be reading this article. Or maybe you just like the pictures.

This is my puppy his name is Donald he is learning to programme a G71 woofing cycle.

Lets take another look at the code.

G0 X21. Z3.
G97 S1200 M3

G76 P010060 Q20 R.02
G76 X16.93 Z-25. P1535 Q485 F2.5

The spindle starts at 1200 rpm and the feedrate (which in the case of a thread is the pitch) is 2.5 mm per rev.

2.5 x 1200 = 3000

So the machine will be feeding at 3000 mm per minute along the thread.

So at the start of the thread you have 3 mm of clearance (Z3.)

Therefore in that 3 mm the machine has to accelerate up to 3000 mm per minute.

If it does not accelerate quick enough you will get a pitch error, your thread will be wrong.

Strange Behaviour

Ever had a thread where you can’t get the gauge on then suddenly it goes on only to find the thread is really loose further down?

Maybe you had a pitch error.

Taking it further if I double the speed

G0 X21. Z3.
G97 S2400 M3

G76 P010060 Q20 R.02
G76 X16.93 Z-25. P1535 Q485 F2.5

2.5 x 2400 = 6000

Now I need to feed at 6000 mm per minute so this pitch problem will be twice as bad.

Can you see where this is going?

Eat more fish.

No not really, well it is good for you but it’s not what I meant.

The faster you go and the courser your thread pitch the quicker the machine will have to feed.

If you have a coarse pitch thread in aluminium you probably will end up with a super high feed-rate your machine can’t even achieve.

This will all depend on the age of your machine but you must always make this calculation just in case you are trying to cut a thread at the speed of light.

G76 threading start point in Z Axis

This start point distance is really important because it will allow the machine to get up to speed.

I can’t give you exact figures for this, not because I can’t be arsed but because it will vary depending on your machine.

The machine will have a maximum feedrate and it will be in the manual.

You know that old book that you use to prop  the door open.

The bigger you make this Z figure the more time your machine will have to get up to speed.

So don’t forget if you are starting at Z1. then the poor old machine doesn’t have much time to get up to speed.


G76 threading start point

Thanks for watching and reading

If you have been affected by any of the issues in this post or need CNC Counselling then contact me.

Siemens 828 840 Sinumerik Training

Or call us

If you want to learn to programme CNC Milling Machines

Look no further Contact CNC Training Centre


I Love Guide i

Category : New Stuff News

Now I know in the past I have been inclined to say some pretty rude things about Fanuc Manual guide.

Well today I’m here to make amends please Mr Fanuke, as the Americans call him, forgive me it was pure ignorance.

Right now that’s out the way. I could write a massive blog about all the shit things but no there are some great things.

I think the more you learn about something the more you seem to like it. Like all these people who slag off electric cars, funny how they have never actually bought one. I have one and I love it.

Let me make a amends today so it;s official “I Love Guide i”

Manual Guide i is great for editing, fixed forms are awesome and graphics are less crap than all the others.

I Love Guide i, Some things you might not know

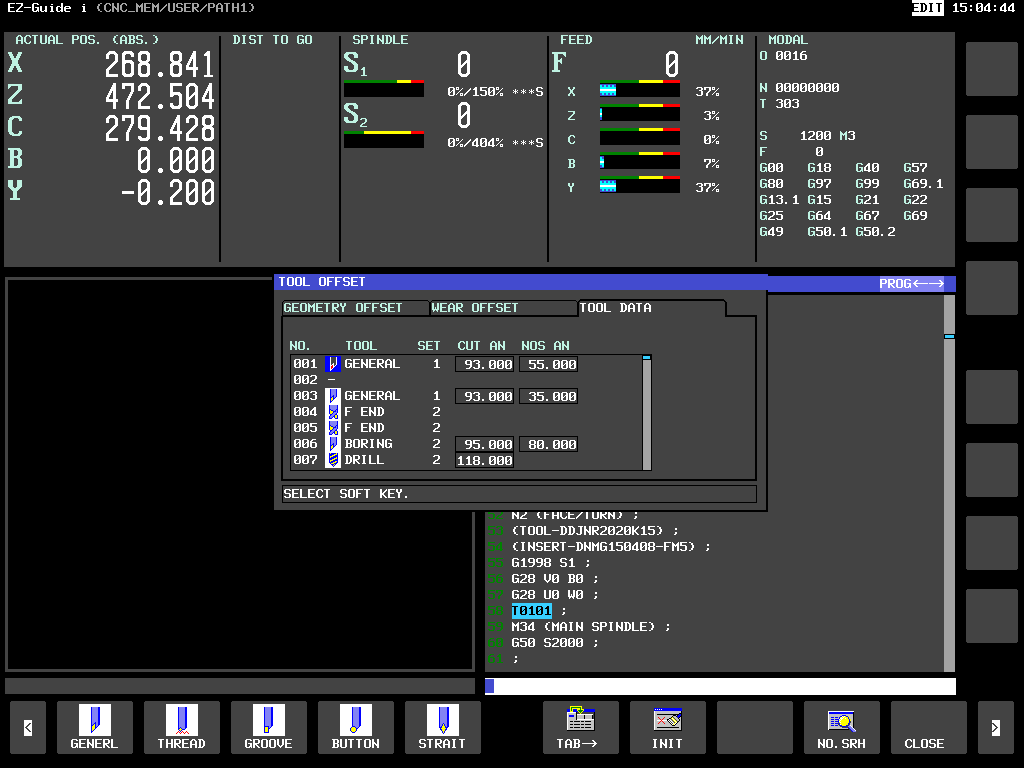
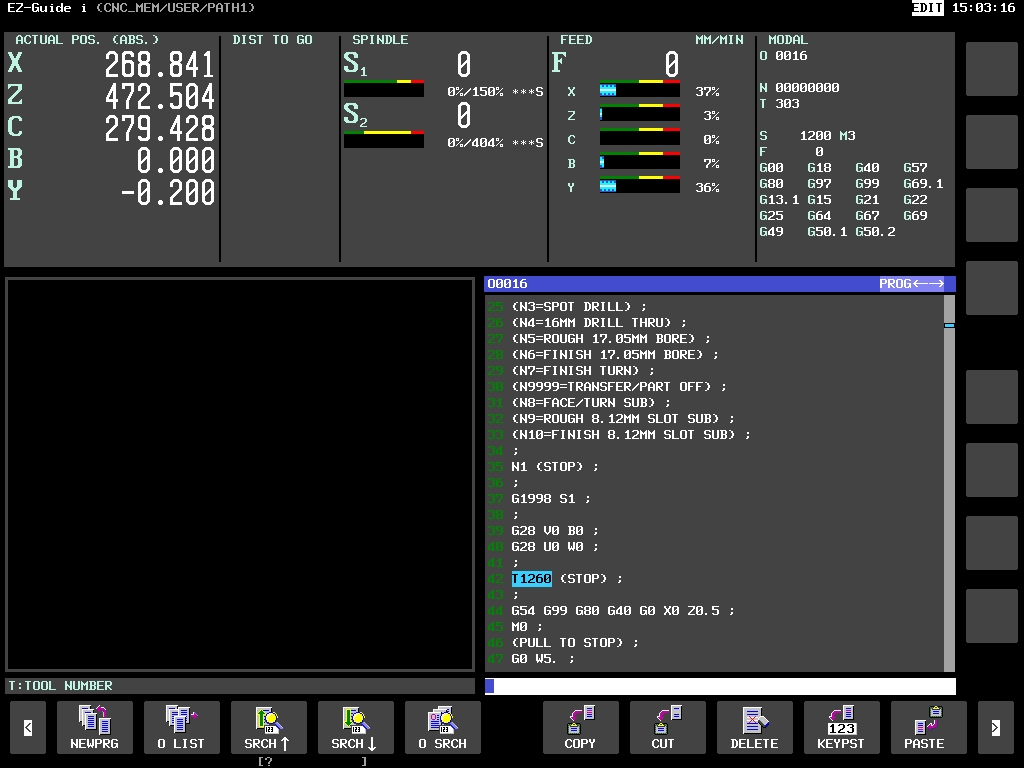
You can click on a tool like in this picture T1260 then press INPUT

I Love Guide i

And it will jump to the tool file.

I Love Guide i

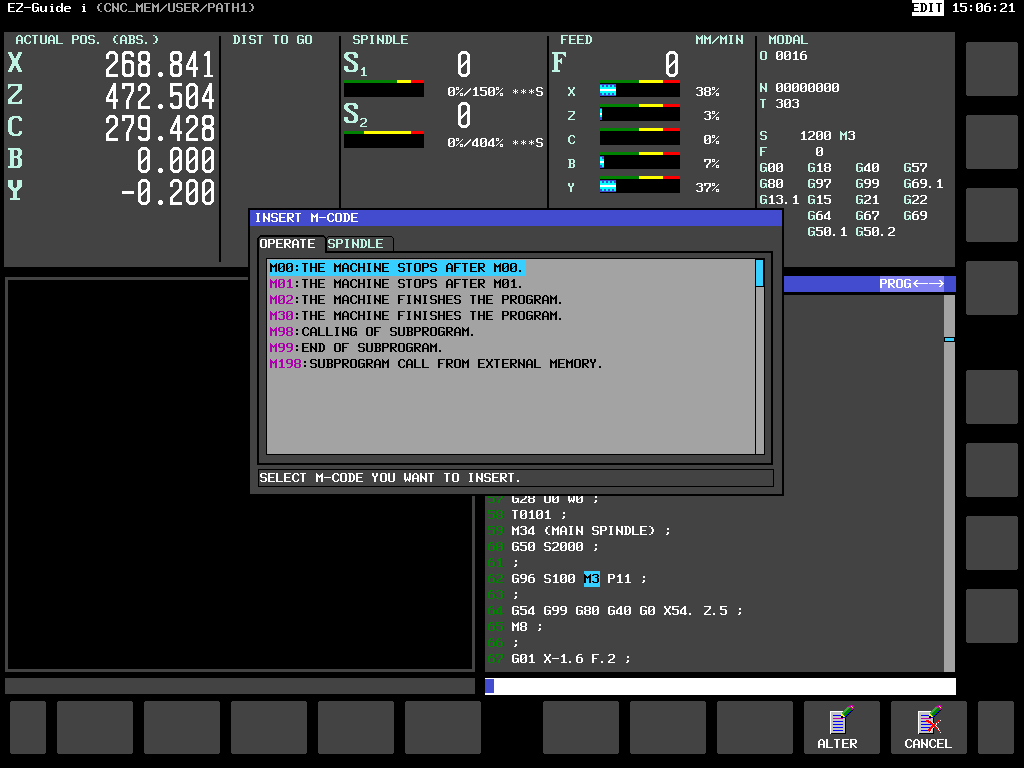
Now try clicking on an M code and press INPUT.

I Love Guide i

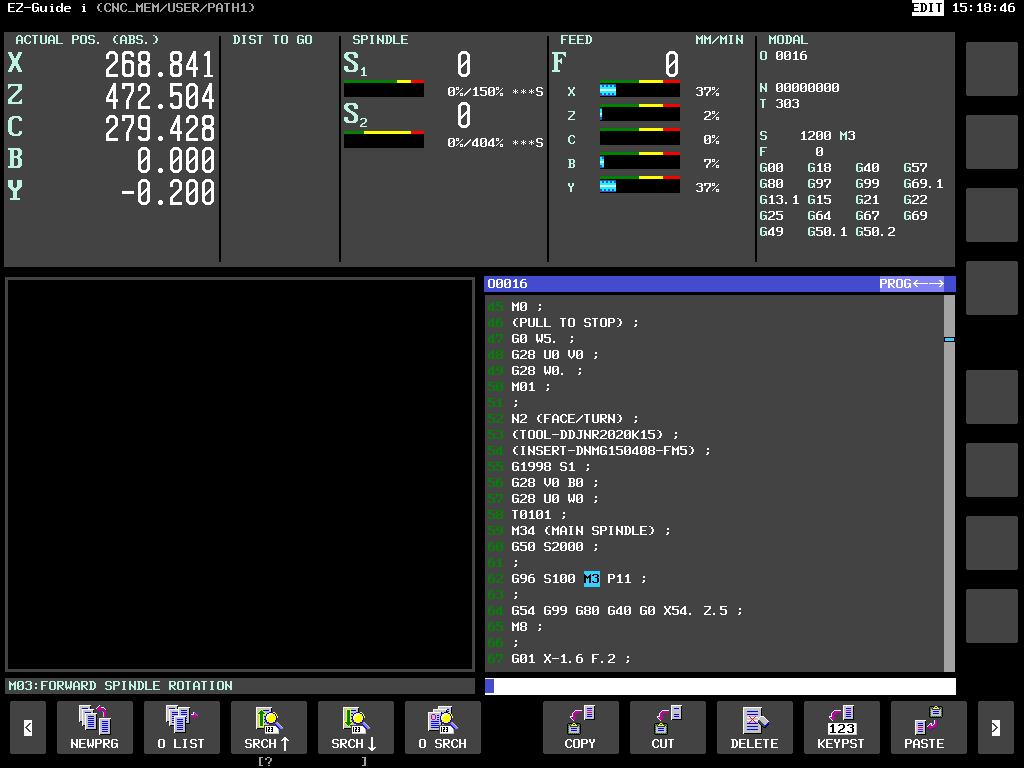
Wow an M code list comes up. I recon that’s impressive and very useful to boot.

I Love Guide i

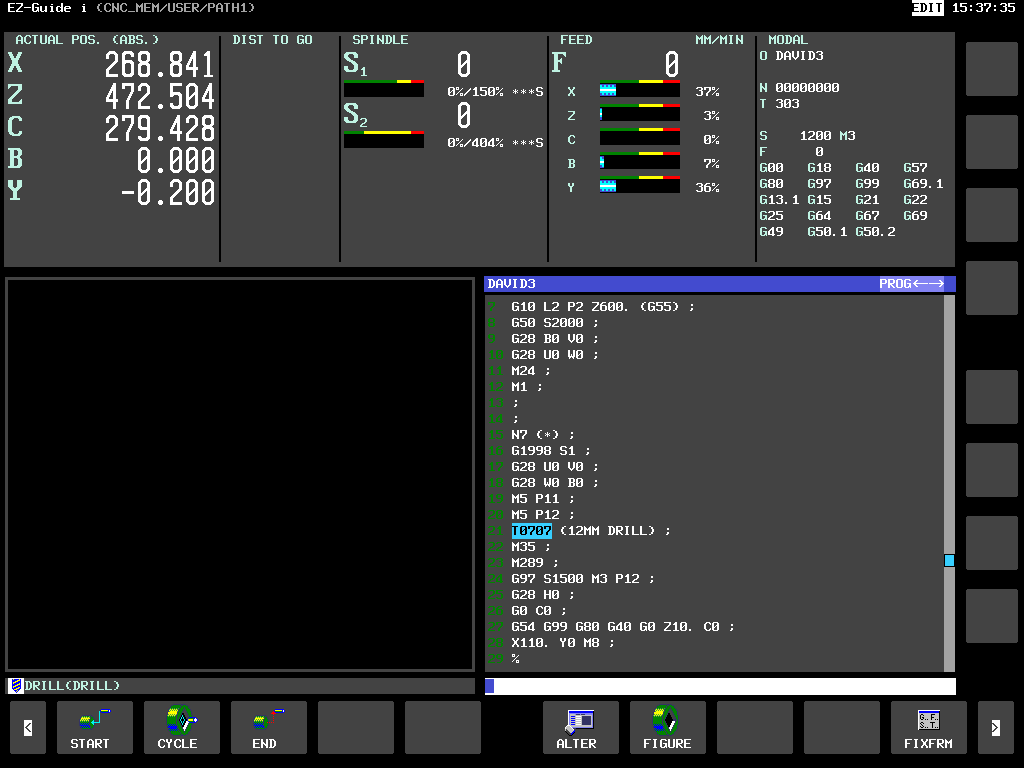
I you have it and you don’t use it then you bloody well should. another reason is that when you click on a G code or M code down the bottom left it tell you what it is. Don’t you just love it. Oh and one more thing if you can be arsed to put all your tool descriptions in it will tell you what they are too.I Love Guide i

Stick around to learn more


Haas CNC Control – What’s Improved and What Still Works

Category : Haas New Stuff

Haas CNC Control – Still Some Clever Ideas After All These Years

I first started training people on the Haas CNC control back in 1995, and at the time it was an absolute game changer.

Not quite in the same way as when I first saw Mazatrol, the Mazak conversational software, which was stunning to say the least. Haas impressed me for different reasons.

What Haas effectively did was take the familiar Fanuc-style control and put it on steroids. A very clever move.

Editing was miles better. Copy and paste — wow! Programs were easy to copy, and program restart was, and in my opinion still is, one of the best systems around. Compare that with Fanuc, where restarting a program can still feel unnecessarily painful.

On a Haas, you could move the cursor to where you wanted in the program and hit Cycle Start. Simple.

And then there were the little things.

When an axis reached the end of its travel, it just stopped. No alarm-induced panic, no turning on the smoke alarms or sprinkler system. It just plain old stopped.

I’m also pretty sure Haas were one of the first to fit a coolant wash-down hose as standard. Ostensibly this was for cleaning down the machine, although its more important use was soaking your unsuspecting mate on the machine next door.

It even had a tray for your coffee cup and a clip for the airline. Someone had clearly spent time using the machine tools Gene Haas I think.

Tool changing was easy too. No M6 T1 followed by an end-of-block. Just input T1 and press ATC Forward.

Fanuc, meanwhile, can seemingly find a way of punishing you for forgetting an EOB.

Haas CNC control


Has the Haas CNC Control Lost Some of That Innovation?

All that said, I can’t help thinking that some of that original innovative approach became a little jaded over the years.

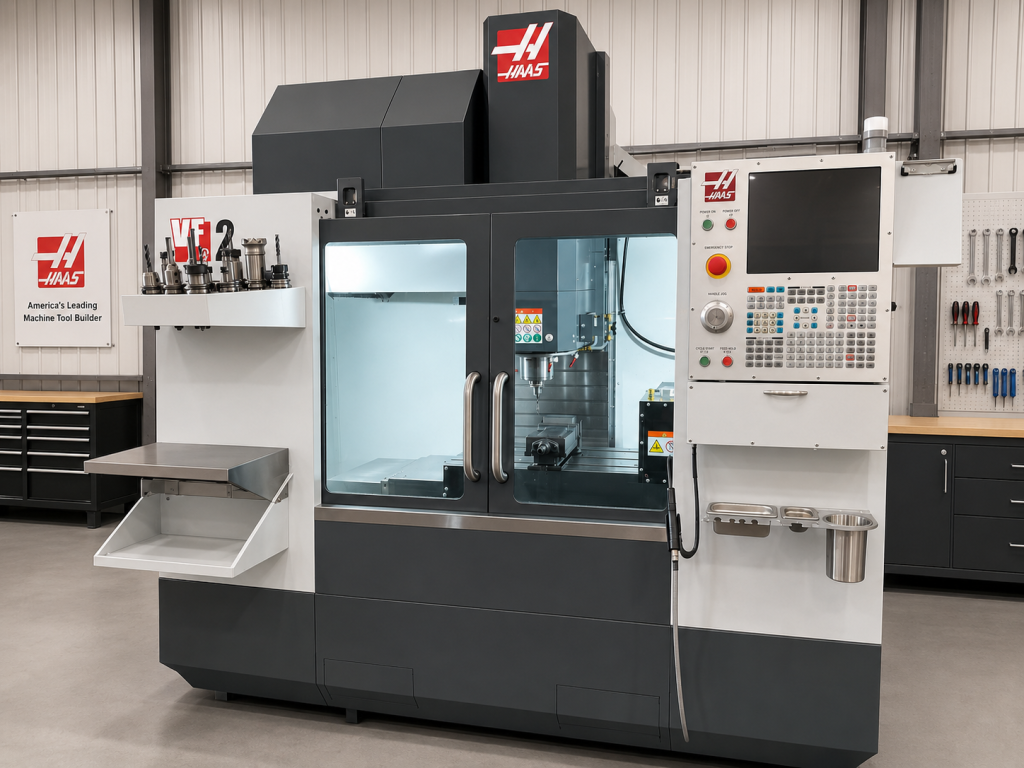
However, I recently worked on a very new VF-2 and noticed a few rather clever features that I really liked. I don’t know how long some of these have been available, but they certainly caught my attention.

“Read More”

Manual Lathe Warco GH 1439

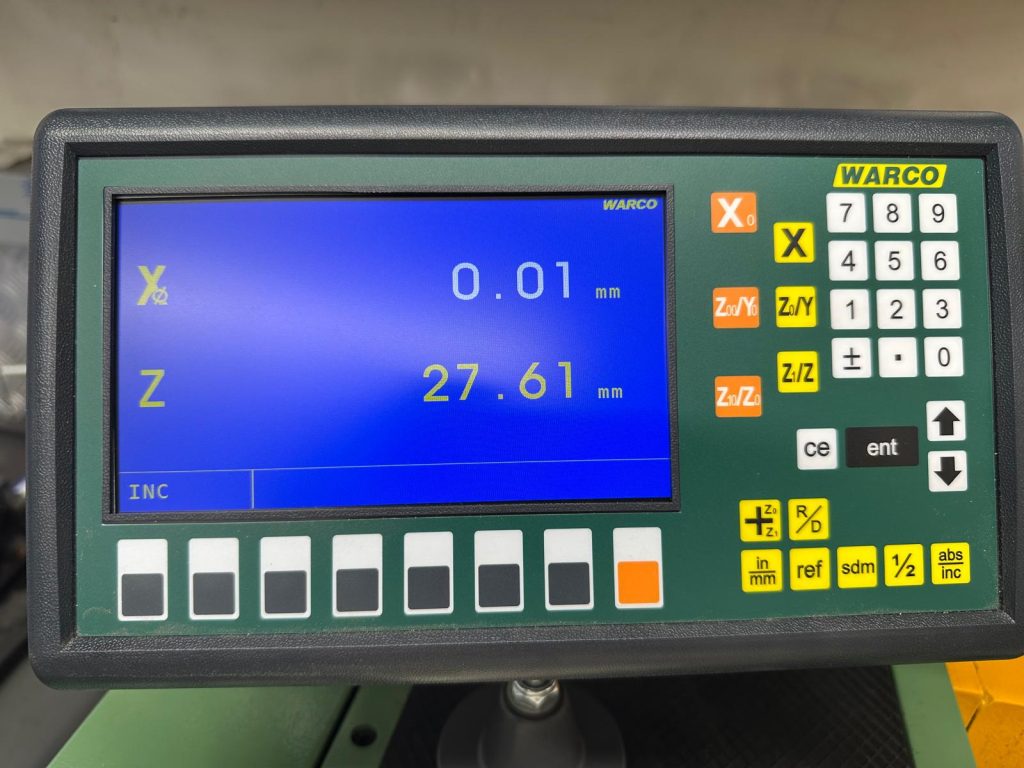
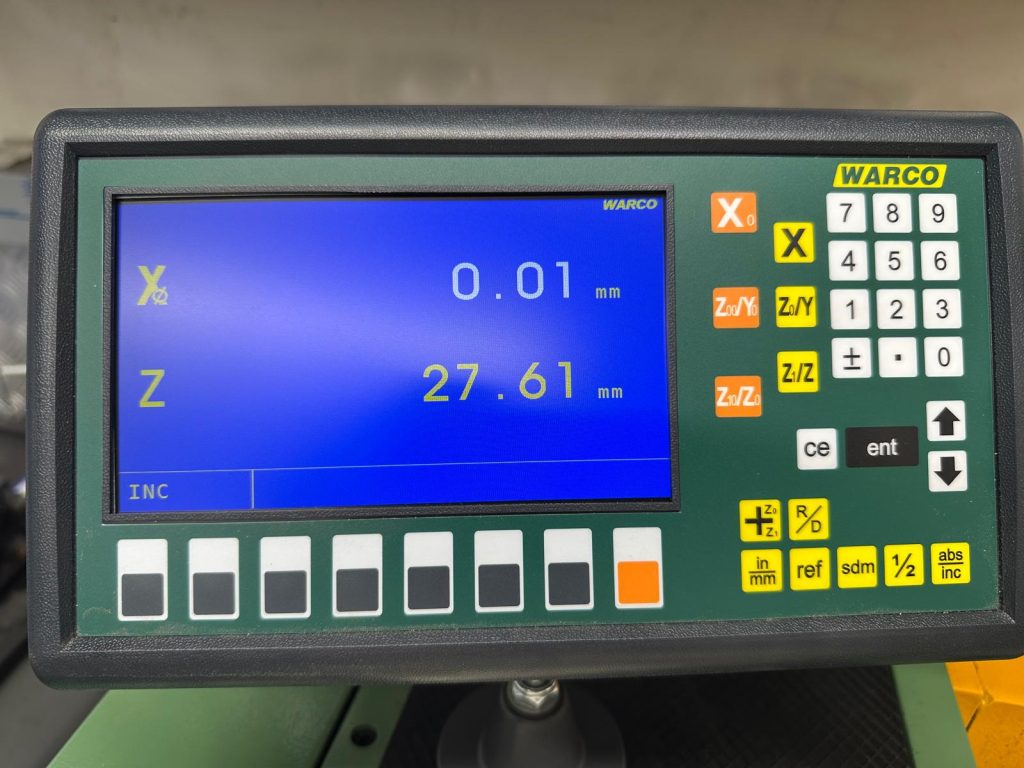
Makes a pleasant change to go back to basic on a simple manual lathe with a DRO (Digital Readout).

I think simple is definitely the wrong word as the level of skill needed to operate this little beast is very high. We are talking years of practice and developed skill.

Now I’m definitely gonna get trolled for this but most of the skill is no longer needed, just buy a CNC.

It is much better when you have a readout DRO (Digital Readout).

DRO (Digital Readout)

Trolled? I don’t even know what it means I just know it’s a bad thing on the internet and it hurts. The only troll I know of is in a fairy tale I used to read to my children. 
Great story about some geezer under a bridge terrifying kids, what could be better?

Yes so sometimes it’s hard to let go of some of these hand skills we don’t need. But what these machines definitely do well is get you used to cutting metal and the overall feel of it.

If it’s a hard material you fuckin know.

Switch It On This Manual Lathe with DRO (Digital Readout)

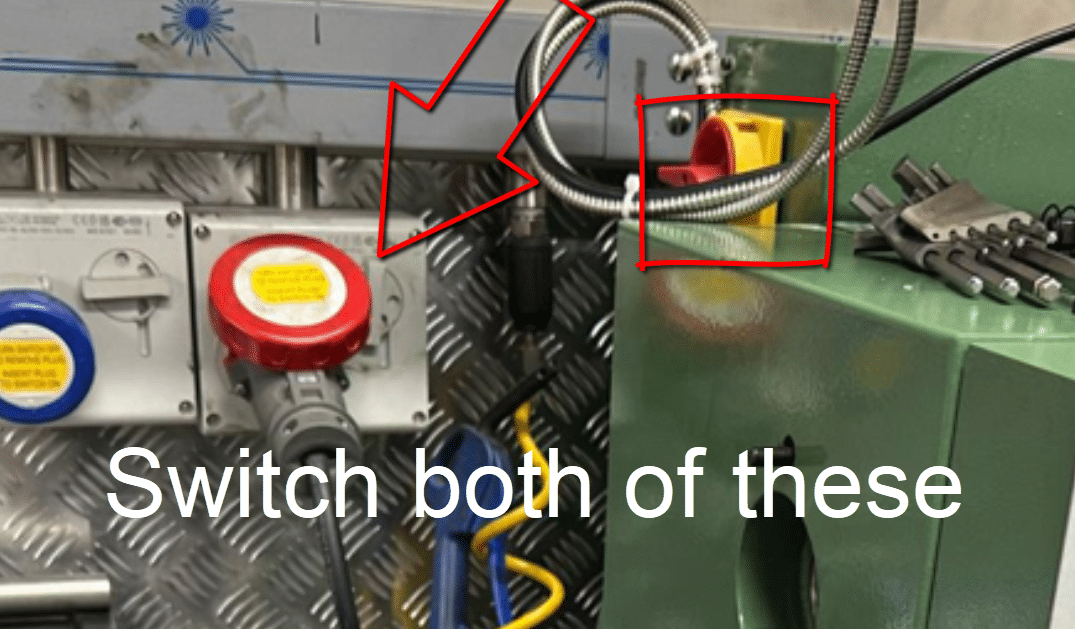
To turn on this machine is easy just flick the isolator round.Manual Lathe

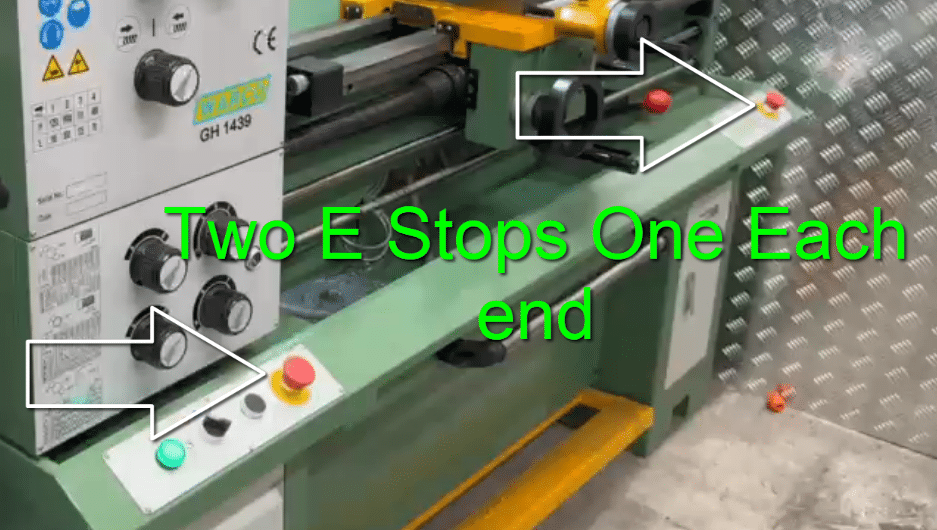
Make sure both Estops are cleared there is one at each end, rotate to release.

The DRO (digital readout has its own switch at the back you may need to flick this over, and after a few seconds it will burst into life.

Safety First

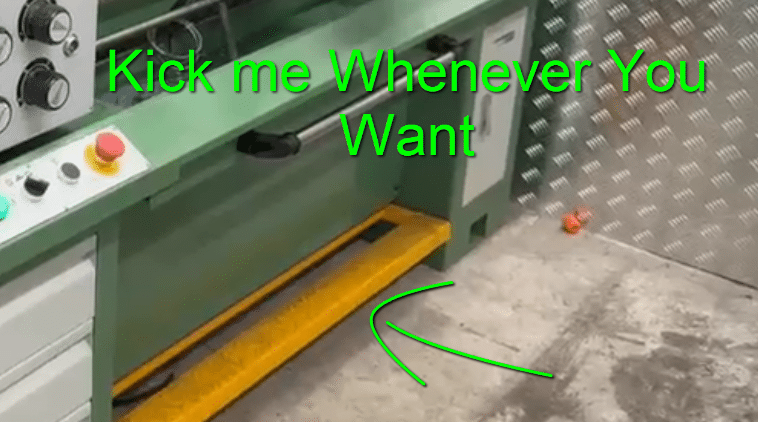
The yellow pedal is your big mate on a Manual Lathe. Press him at anytime and the machine will stop dead. In any dodgy situation keep your foot over this ready.

“Read More”

G130 Doosan Lynx 300M – Set the G30 Position

Category : New Stuff

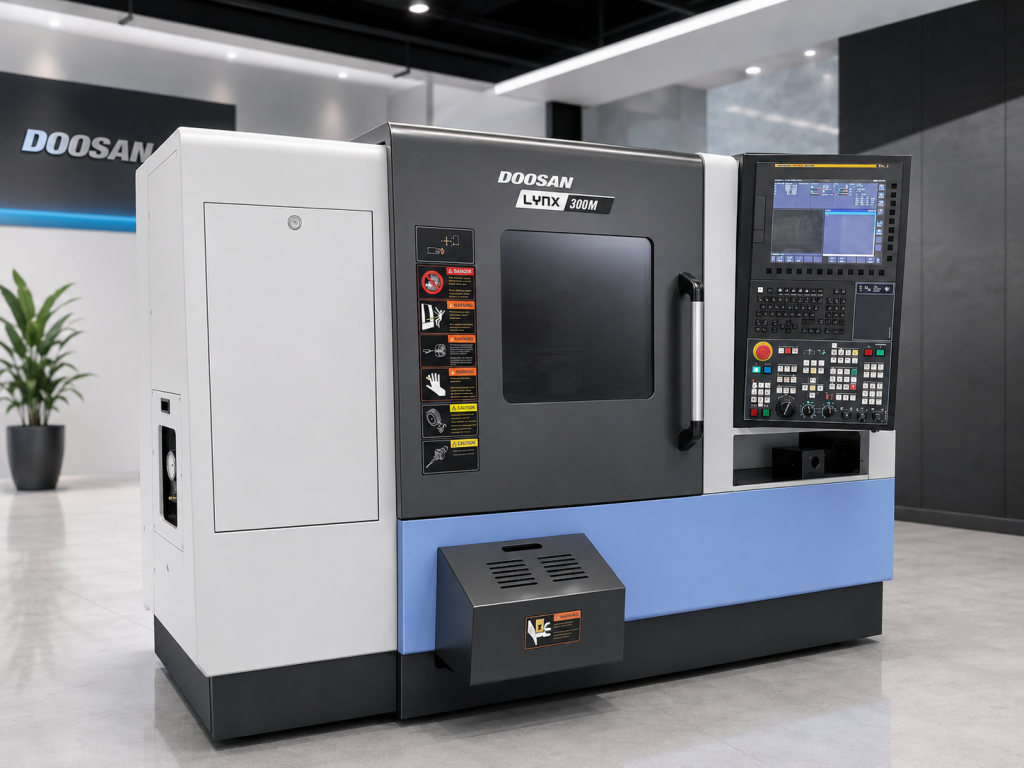
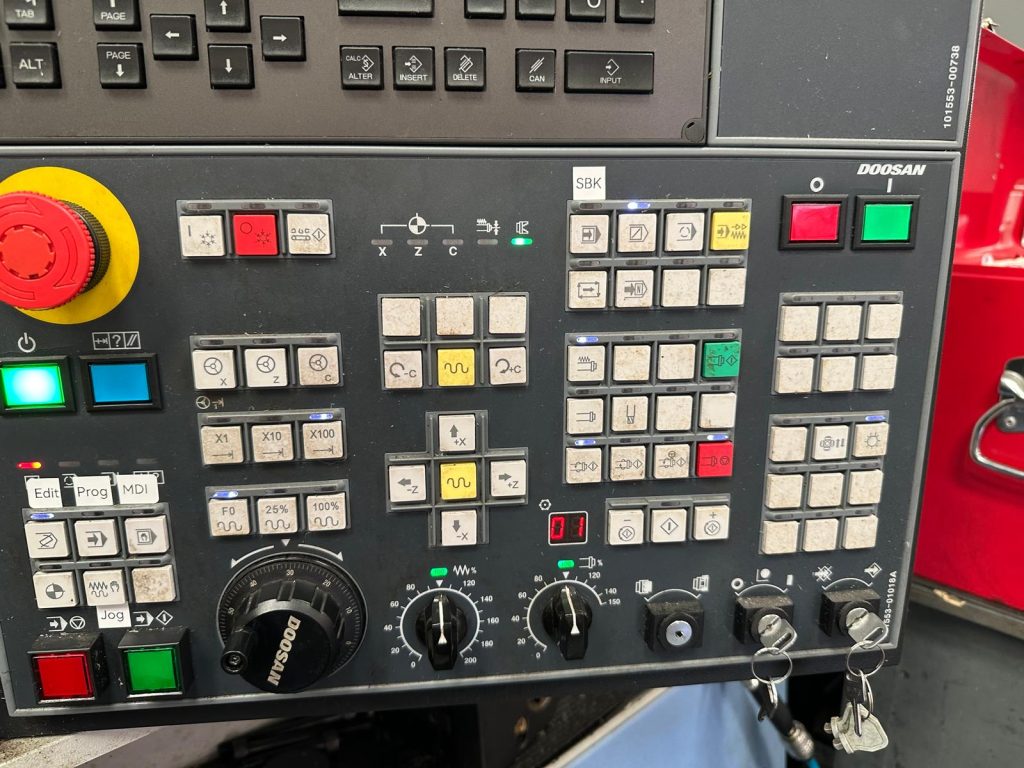
G130 on a Doosan Lynx 300M – Setting the G30 Position

Doosan Lynx 300M G130

On a Doosan Lynx 300M, G130 can be used to set the machine’s G30 second reference position.

The interesting part is that G130 is not doing the work itself.

Read on if you are scared of fucking with parameters.

On this machine:

G130

calls:

O9019

This is done using Fanuc parameter 6059.

If parameter 6059 contains:

130

then G130 calls macro O9019.

Doosan Lynx 300M G130

What Does O9019 Do?

The macro reads the position you added to G130 and writes it into Fanuc parameter 1241.

Parameter 1241 stores the second reference position, normally associated with:

G30 P2

So instead of manually entering the position into parameter 1241, you can enter it on the G130 line:

G130 X200. Z200.

Simple.

This is called a G Code Alias read about it here

How It Works

G130 X200. Z200.
↓
Parameter 6059
↓
O9019
↓
Your X200. Z200. position
↓
Parameter 1241
↓
G30 second reference position

Setting the Position

  1. Reference the machine.
  2. Jog the turret to the required position.
  3. Check that the position is safe.
  4. Record the existing parameter 1241 values just as a safety precaution.
  5. You could even take a screen shot.
  6. Add you new position to G130 for example G130 X200. Z200.
  7. Check parameter 1241.
  8. Test the G30 move at a low rapid override.
  9. (G30 U0 W0)

Why Use G130?

It is quicker than manually typing coordinates into parameter 1241 and reduces the chance of entering the wrong value.

It also gives the setter a very simple command:

G130 X200. Z200. (set my G30 position here)

It’s Permanent

Yes it stays in forever unless you change it. Therefore you don’t have to keep writing G130 in a program if you always use the same position.

If you are scared of fucking with parameters then this is your answer. Change the G30 position and no one dies.

Important

G130 is a custom G-code alias on this machine. Do not assume it performs the same function on every Fanuc-controlled machine it will not.

This is a Doosan specific command. Now you know how you could add it to any machine, see end of article for full code.

Also, back up your parameters and macros before changing anything.

“Read More”

Careers in CNC

View all current vacancies in CNC

Click here

Call David: 07834 858 407