
Fanuc G73
Call David: 07834 858 407
for Hurco training
Anyway here is a little thing about a Hurco control that is really useful. One of the things I always teach my pupils, or victims as they are sometimes called is this.


Anyway here is a little thing about a Hurco control that is really useful. One of the things I always teach my pupils, or victims as they are sometimes called is this.
I’ve wanted to get my hands on a new Haas machine for a while. Really wanted to see what the new control was like.

Stiltz provided the machine and the victims for the training.
If you have read any of my articles you will know I have always had an affection for Haas machines. The first one I ever worked on being about 1994. At that time they were nothing short of ground breaking innovation.
Things like a built in airline and coolant wash-hose were not only innovative but really useful.

A machine that worked straight out of the box. Easy peasy tool-change. Handwheel to scroll through the program, people still get impressed by this today.
Programmable coolant nozzles, fuckin hell that was a game changer. Just move nozzle to a position and press an F key and it’s stored with the offset.
Macro at no extra cost (wow) some people wanted two grand for this (cost of a good family car in 1995)
Program restart still the best in the world, don’t get me started.
To start with on this one I didn’t like the interface but it does grow on you. You need to get used to using the touch screen. Access to some menus is a bit convoluted too.
This Haas Mini Mill has a 10k spindle and 30 tools.
Something I suddenly remembered about this model. Well you know when you get a cup of coffee and it’s in a tall tapered glass mug? You are thinking “nice big cup of coffee”. You take four big swigs n it’s gone, shit what happened. What happened is an optical illusion because the cup is tapered it’s actual capacity is that of a thimble.
It happens all the time everything comes in a great big box with loads of packaging and the actual item is minute.
Anyway try moving this machine to the end of it’s stroke in X. Fuckin hell what a disappointment I recon you can only move around about half the table. I mean great you can put a pretty big part on here. That’s great so long as you don’t want to machine it!!!
It definitely is not what you expect from the company that’s known for pragmatism. Anyway that does piss me off.
The way this machine is being used is running programs from a memory stick. At first I thought it was a bit crazy as the programs weren’t particularly big.
Anyway surprise surprise it works well. Just plug in and press load and it runs. But what about editing you ask. No problem you just do it. Same as normal.
Program restart, no problem works exactly the same as when running from memory.
This week I got to train two people on a Haas VF3, and what a delight it was. This machine was old I mean 1996 but still a great functional machine tool.
I like to see myself in a similar way, really old but still functioning, well at least as I write.
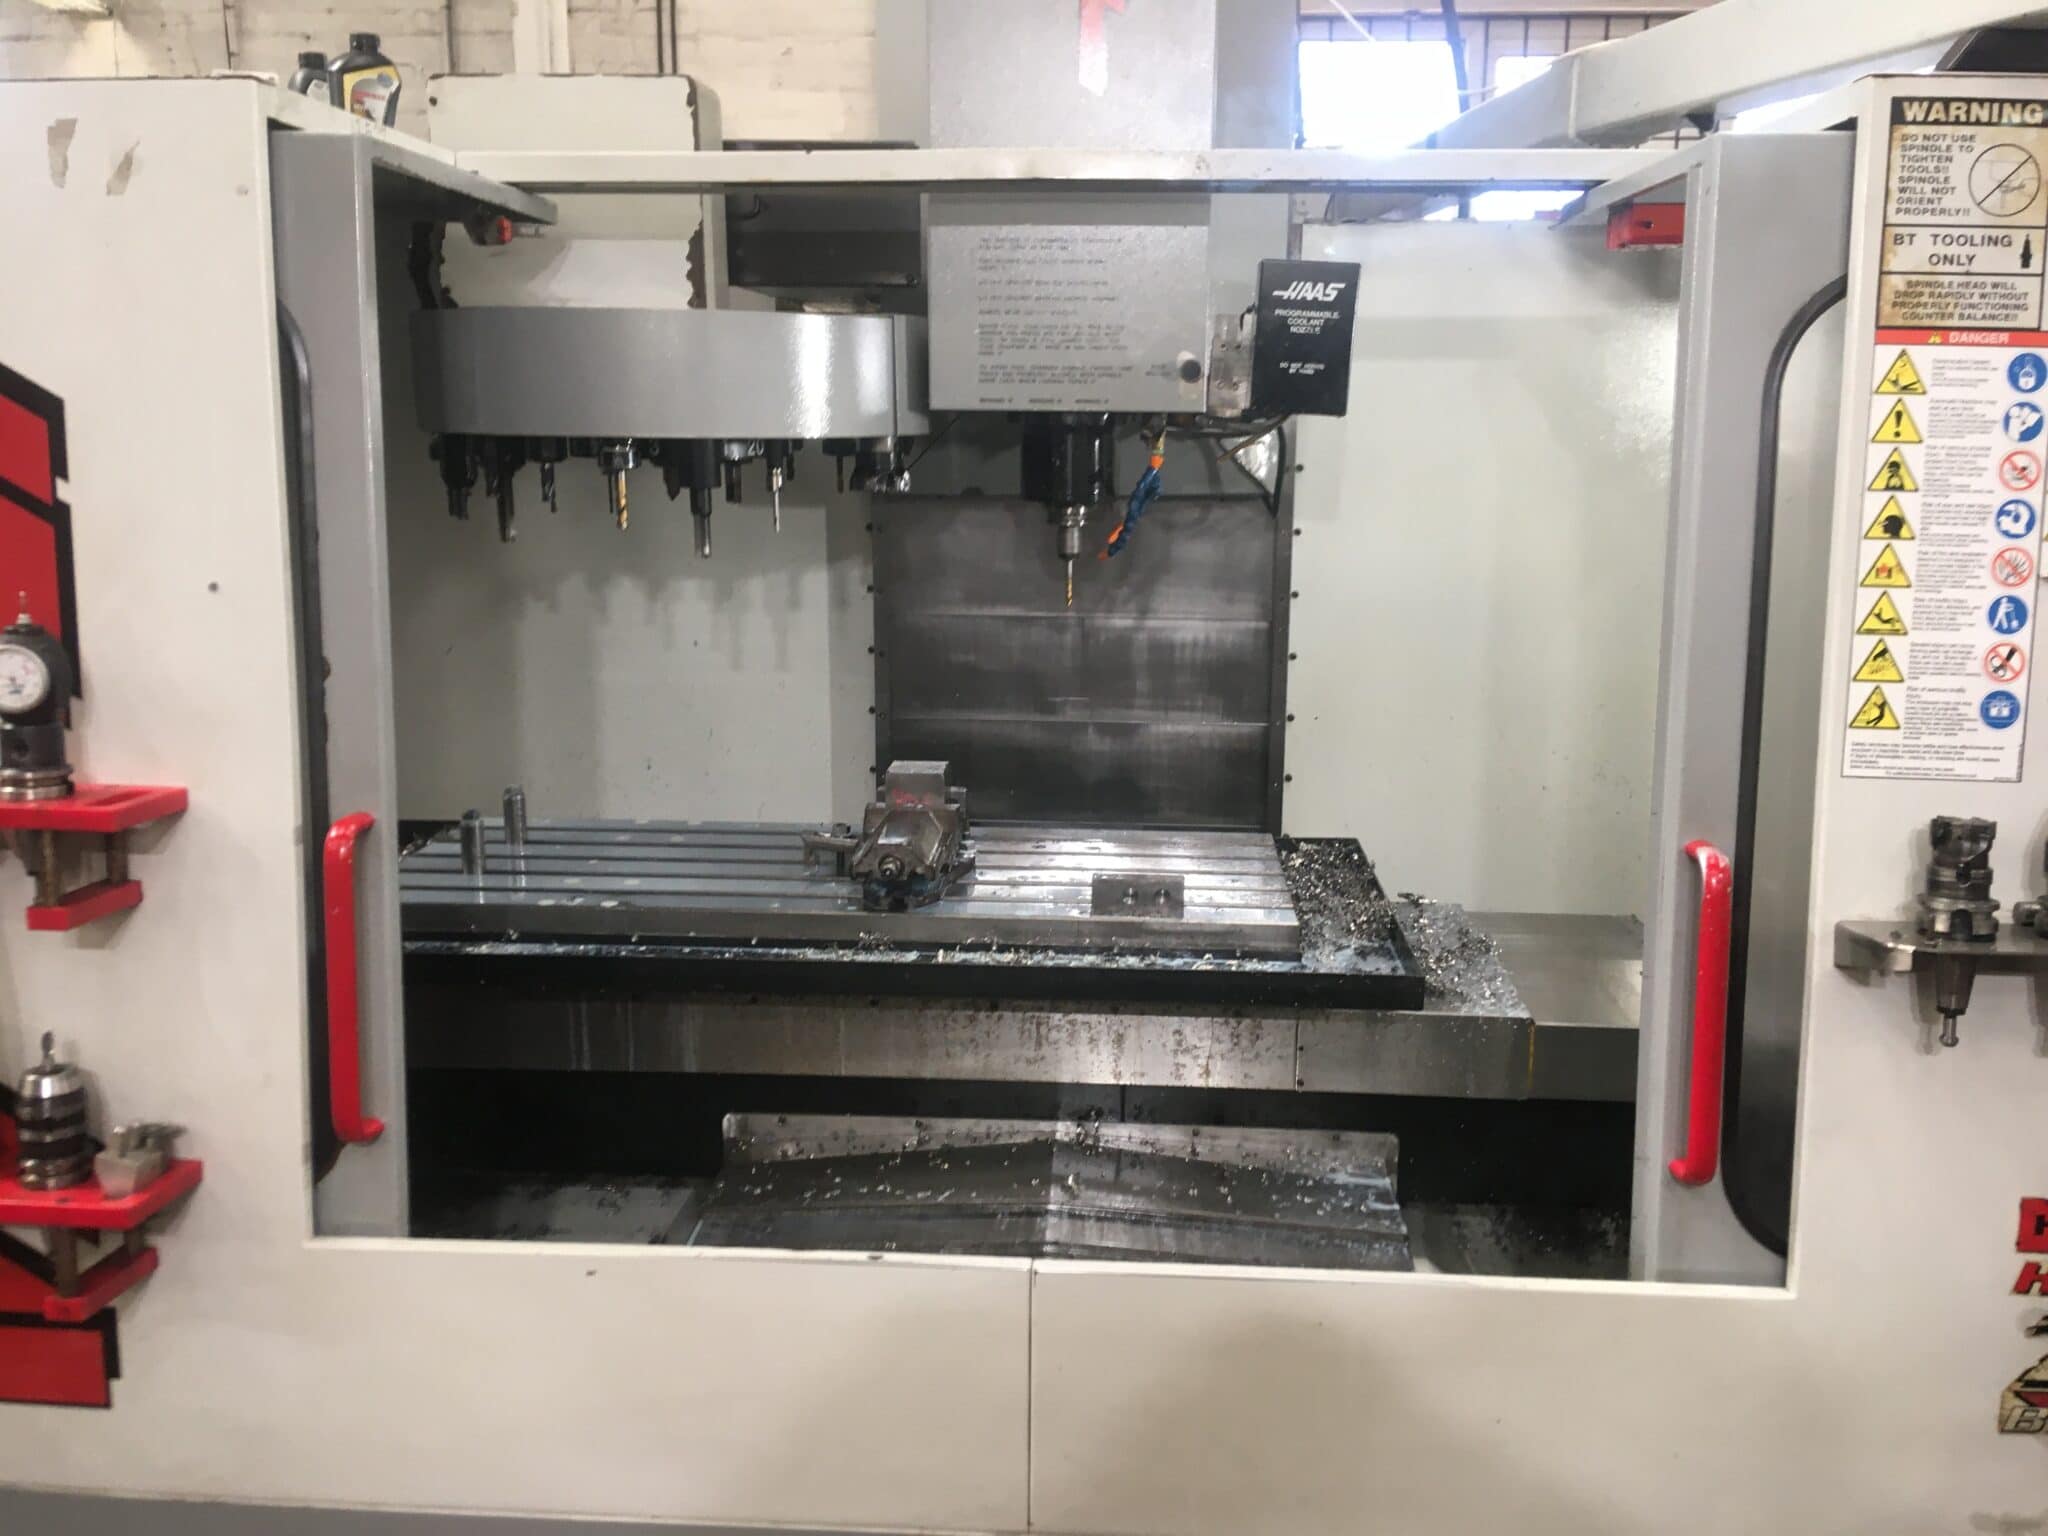
It took me back to when I first set up my business of training people on CNC machines. My first two victims were at Armitage Shanks in good old Wolverhampton.
1996 was the year I started out on my own CNC Training and these were the first machines I trained on. I did so many I got pissed off with the sound of my own voice (which I rarely do).
Because all the machines were the same I was saying the same things and quoting the same tired old anecdotes day after day.
Fortunately, I went on to train on all the well-known CNC machines like Mazak, Mori Seiki, Matsuura, Bridgeport to name a few. Quite a lot of the not so well-known ones like Maho, seen below.

The machine above has a Phillips control and they were the absolute dogs’ bollocks. It even had rigid tapping. You could hit feed-hold while it was tapping and you got the option to reverse the tap out! Training people on these was an absolute delight.
Don’t forget we’re talking mid 80s here.
Shut up David this sounds like a big plug for the CNC Training Centre, or maybe it is.
There is pub by us and on the sign, it says “The Home of the Roast”.
You have to queue up to get your food and a young lad carves the meat in front of you. If he don’t like the look of you, which obviously with me he didn’t, you get two or three slices of turkey, so wafer thin, you can see the pattern on the fuckin plate underneath.
Now I don’t want to knock the people of Nuneaton, being as most of my family live there, but honestly there are some greedy bastards about.
After you get your meat and a few accoutrements you follow a long line of people adding cabbage and peas and all sorts of vegetables and potatoes to their plates. This bloke in front of me was scooping so much on to his plate it was flowing over. It was like a fuckin bowler hat as my late father would say, sans expletive.

In those days you didn’t swear in front of ladies, unless of course it was their turn.
I was just thinking “did you like not eat for a fuckin week?” You can imagine his kids at school saying to the teacher “oh, we’re not eating at our house this week miss”. The teacher then asks if this is some precursor to a religious festival or some such thing.
“Oh no miss, we’re booked in at the carvery for Sunday lunch” she gives them a knowing nod.
Anyway, I looked at this blokes plate with utter middle class disgust and vowed never to go there again.
My mate was about three people in front of this bloke and to my amazement my mate’s plate was so full of food, it made his look like he’d paid for the children’s menu.


Haas products are constantly improving and developing. I love working with Haas because they actually listen to customers.
Every company claims to do this. We all know that some of the software and machines we use everyday have annoying faults that just never seem to be picked up on by the designers.

Anyway you all know I get pissed off about this if you ever read anything I write. Here is an example.
Did you ever work on a machine with a random tool-changer?

This is a CNC Milling machine that gets the tool out of the spindle and puts it back into the nearest pocket. Could be a Fanuc control Mazak control, Heidenhain. So when you look round the back of the machine at the pockets, the pocket numbers bear no resemblance to the actual tool numbers.
Anyway you go round the back of the machine and you see a tool you want. An M10 tap maybe. I want that M10 tap so I have to go all through my tool lists or whatever to find what tool number it is.
I hope you get me so far. So I find there is an M10 tap called T06 and I call it to the spindle. Oh dear there are two M10 taps and I got the wrong one. In real life I would probably say bollocks but I am trying to make these articles more classy by reducing the profanities.
Today I got to train someone on a Haas SL15 Lathe, it had live tooling and a sub spindle.

It also had a bar-feed.
Not worked on one of these for a while. Tell me why on earth don’t other companies look at the pragmatic approach that Haas take to CNC Machining and copy it?
Say what you like about Haas machines but they have an incredible knack of shattering the bullshit and making stuff easy.
G112
G112 tricks the Haas SL15 CNC Lathe into thinking it’s a machining centre and that it can mill.
It’s like gender identity for CNC Machines. But, and this is the “for fuck sake bit”, on most machines you have to program it like a machining centre but then when your done you need to double X and switch all the Y’s for C’s.
Sounds simple but in practice it’s a shit storm, specially when programming G2 and G3.
When Mr Haas invented the Haas SL15 CNC Lathe he must have looked at this and laughed. Here is a really clever idea. We’ll trick the machine into thinking it’s a machining centre and here is the clever bit. We’ll keep up the facade.

So you make a milling program (XY) and then……. you leave it that way. How incredibly clever is that?? Mmmmmm