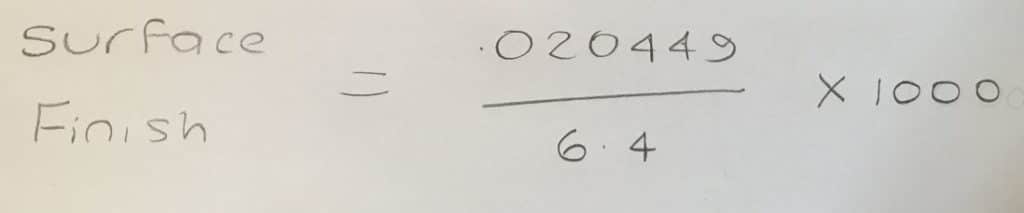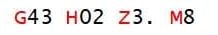Category Archives: Beginners

Surface Finish CNC Turning

Category : Beginners

CNC Turning Surface Finish

Ever wondered what feed rate is best to give you a particular CNC Turning surface finish? Or do you just guess?

Well look no further. From now on you’ll be able to work out what feed-rate will give you the surface finish you require when CNC Turning.

Oh and there’s a formula where you can work out what surface finish you’re going to achieve without a fortune teller.


We are going to use um Ra.

The um stands for microns.

The Ra stands for roughness average.

Here is a full explanation if you really want to know. 
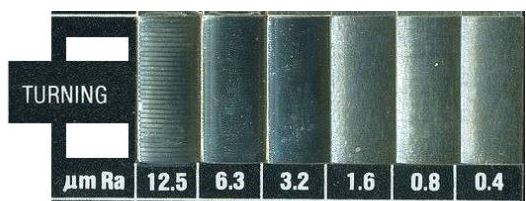
CNC Turning


You can buy a flat block like the one above which you can use as a comparison to see what surface finish you’re getting.

The section above is for CNC Turning surface finishes.

So you can already see that 12.5 is like a plowed field and .4 is like a babies arse (as my father used to say) .

So if you’re fixing a fence post then 12.5 might be OK.

Surface Finish The Dreaded Formula

surface finish

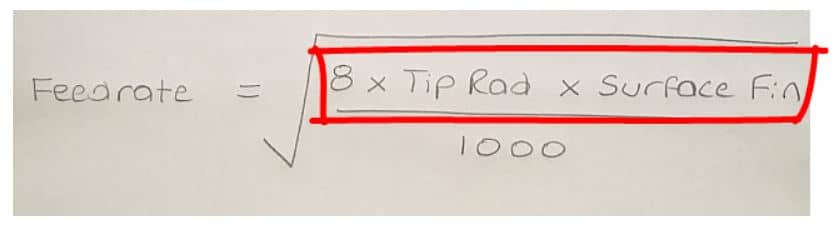
First of all what feed rate would you need to obtain a certain CNC Turning surface finish.

CNC Turning

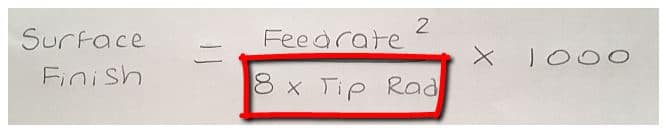
Now what if you’re already machining the part. That means you know the feed rate. What surface finish will you get?

CNC Turning

So………….

Our tip radius is .8mm

CNC Turning

We want to achieve a 3.2 um Ra  CNC Turning surface finish

CNC Turning

So here’s the formula.

CNC Turning

Let’s do this bit first.

https://www.youtube.com/watch?v=vWQgBtlUUMM&ab_channel=MotoMadness

8 x .8 x 3.2 = 20.48

Now let’s divide it by 1000
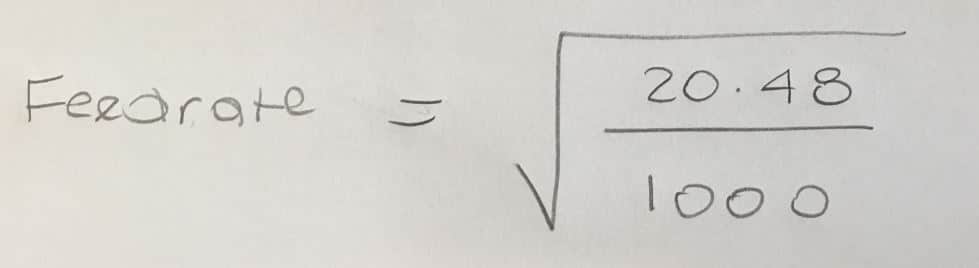
https://www.youtube.com/watch?v=vWQgBtlUUMM&ab_channel=MotoMadness

20.48 / 1000 = .02048

Now lets square root the answer.

https://www.youtube.com/watch?v=vWQgBtlUUMM&ab_channel=MotoMadness

Square root of .02048 = .143

So the feed-rate you need is F.143

CNC Turning

OK… You Came Back. You Ready to Carry On?

Anyway let’s see how you do it backwards.

surface finish

So imagine you had been turning these imaginary bits with a .8mm radius insert at a feed-rate of .143 (F.143)

First of all square the feed rate .143 x .143 = .020449

CNC Turning

Now do the bottom bit 8 x .8 = 6.4

surface finish

Now divide the top by the bottom.

surface finish

.020449 / 6.4 = 0.00319515625

Then simply multiply this by 1000

0.00319515625 x 1000 =3.19515625 (3.2)

That’s 3.2 to you

surface finish
A surface finish comparator

It worked backwards!!! Phew what a relief.

Surface Finish, Now Let’s Think About This

So to get a 3.2 finish with a .8 tip radius you would need a feed rate of .14

Now let’s do the same calculation with a .4 radius tip.
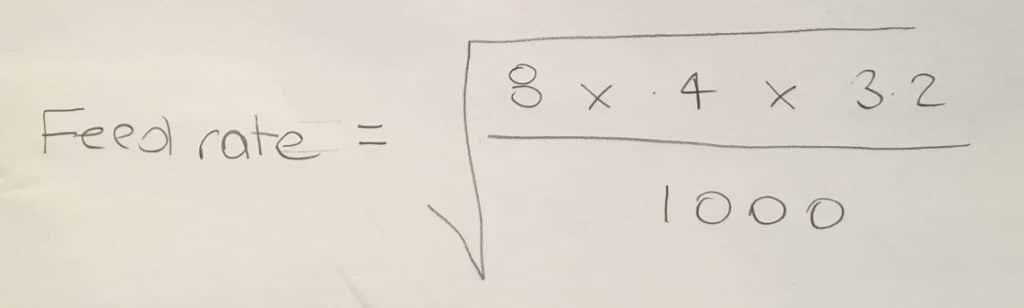
surface finish
Calculate surface finish

So did you work it out?

Here’s one I prepared earlier.

The answer is .101

And if you can be bothered to work it out with a 1.2 radius tip.

The answer is .175

.4    =  .101
.8    =  .143
1.2  =  .175

Interesting

So as the tip radius gets bigger you get to increase the feed rate!

Thanks for watching and reading

If you have been affected by any of the issues in this post or need CNC Counselling then contact me.

Oh yea we do CNC Training too not to mention Classroom Training.

Or call us

If you want to learn to program CNC Milling Machines

Look no further Contact CNC Training Centre


G83 Peck Drilling Program

Category : Beginners Fanuc

G83 Peck Drilling Program Example

G83 Peck Drilling Program, G83 is a deep hole peck drilling canned cycle.

Cycle G83 drills holes breaks up the chips as it goes. It fully retracts from the hole after each peck.

This simple part has four M12 holes drilled countersunk and tapped. The datum is the centre of the part so the holes positions are.

X55. Y55.
X-55. Y55.
X-55. Y-55.
X55. Y-55.

G83 Peck Drilling Program

G83 Peck Drilling Program

Here is the CNC code

G83 Peck Drilling Program

The machine first moves to X-55. Y-55. and rapids the Z axis to 3mm above the part.

G83 Peck Drilling Program

It then rapids the Z axis down to 1mm above the part R1.

The G83 Cycle instructs it to drill a hole 17.5mm deep (Z-17.5) at a feed of 200mm per minute (F200.) 

The Q2. tells the machine to drill the hole in 2mm steps. After each step it retracts to the surface of the part.

This allows all the chips or powder to come out of the hole after each cut. It also allows the drill to cool.

As it drills the depth increases by 2mm each time.

When the hole is done it rapids back to the initial point (Z3.) This was in the line

G83 Peck Drilling Program

This is because of the G98.

If it were G99 it would return to 1mm above the job (R1.)

See explanation of G98 and G99

Once the cycle is active each time it sees a position it repeats the drilling process.

When the G80 is programmed it no longer drills holes.

Now watch the video to see it all in action.

G83 Drilling Program Example

More G83 stuff from Haas

Thanks

If you have been affected by any of the issues in this post or need CNC Counselling then contact me.

If you want to learn to program CNC Milling Machines

Look no further Contact CNC Training Centre


Letter O Head of Programme

Letter O Head of Programme

There is a quick way of doing most things on computers and CNC Machines

It’s just being bothered to first find out what they are but most importantly force yourself to keep using them until it becomes habit.

To get to the head of your Fanuc Programme type in letter O and press your upper cursor.

Letter O Head of Programme

It beats the shit out of pressing reset which can stop everything if you press it by accident.

Classroom Training

Mazak Training


Careers in CNC

View all current vacancies in CNC

Click here

Call David: 07834 858 407